Design for Manufacturing has a reputation problem. Engineers hear "DFM" and assume it means compromising the design to make life easier for the shop floor.
It's the opposite. Good DFM removes cost that was never buying you anything — tolerances no function requires, features no cutter can reach, custom parts where a catalogue part would do. The part performs identically and costs substantially less.
Here are seven rules we apply to every project, and why each one matters.
1. Question every tight tolerance
Tolerance is the single biggest cost lever in machining. Moving a dimension from ±0.5 mm to ±0.01 mm can multiply the cost of that feature several times over, because it changes the machine, the tooling, the fixturing, and the inspection.
The test is simple: what does this surface actually do? If it seals, slides, locates, or carries a press fit, tighten it. If it just exists, open it up. On most parts, a small minority of features drive the majority of the machining cost — and they're almost always the tightest tolerance and the deepest pocket.
2. Design internal corners a real cutter can make
Every internal corner in a machined pocket has a radius, because end mills are round. Specifying a sharp internal corner means either EDM, a broaching operation, or a very slow small-diameter cutter — all expensive.
Give internal corners a radius at least slightly larger than the cutter you expect to be used. A generous corner radius also lets the machinist use a bigger, stiffer tool and take heavier cuts, which cuts cycle time.
3. Keep wall thickness uniform and workable
Thin walls chatter. A wall that's fine at 4 mm may vibrate uncontrollably at 1.2 mm once the pocket beside it is cut, producing poor finish and potentially scrapping the part.
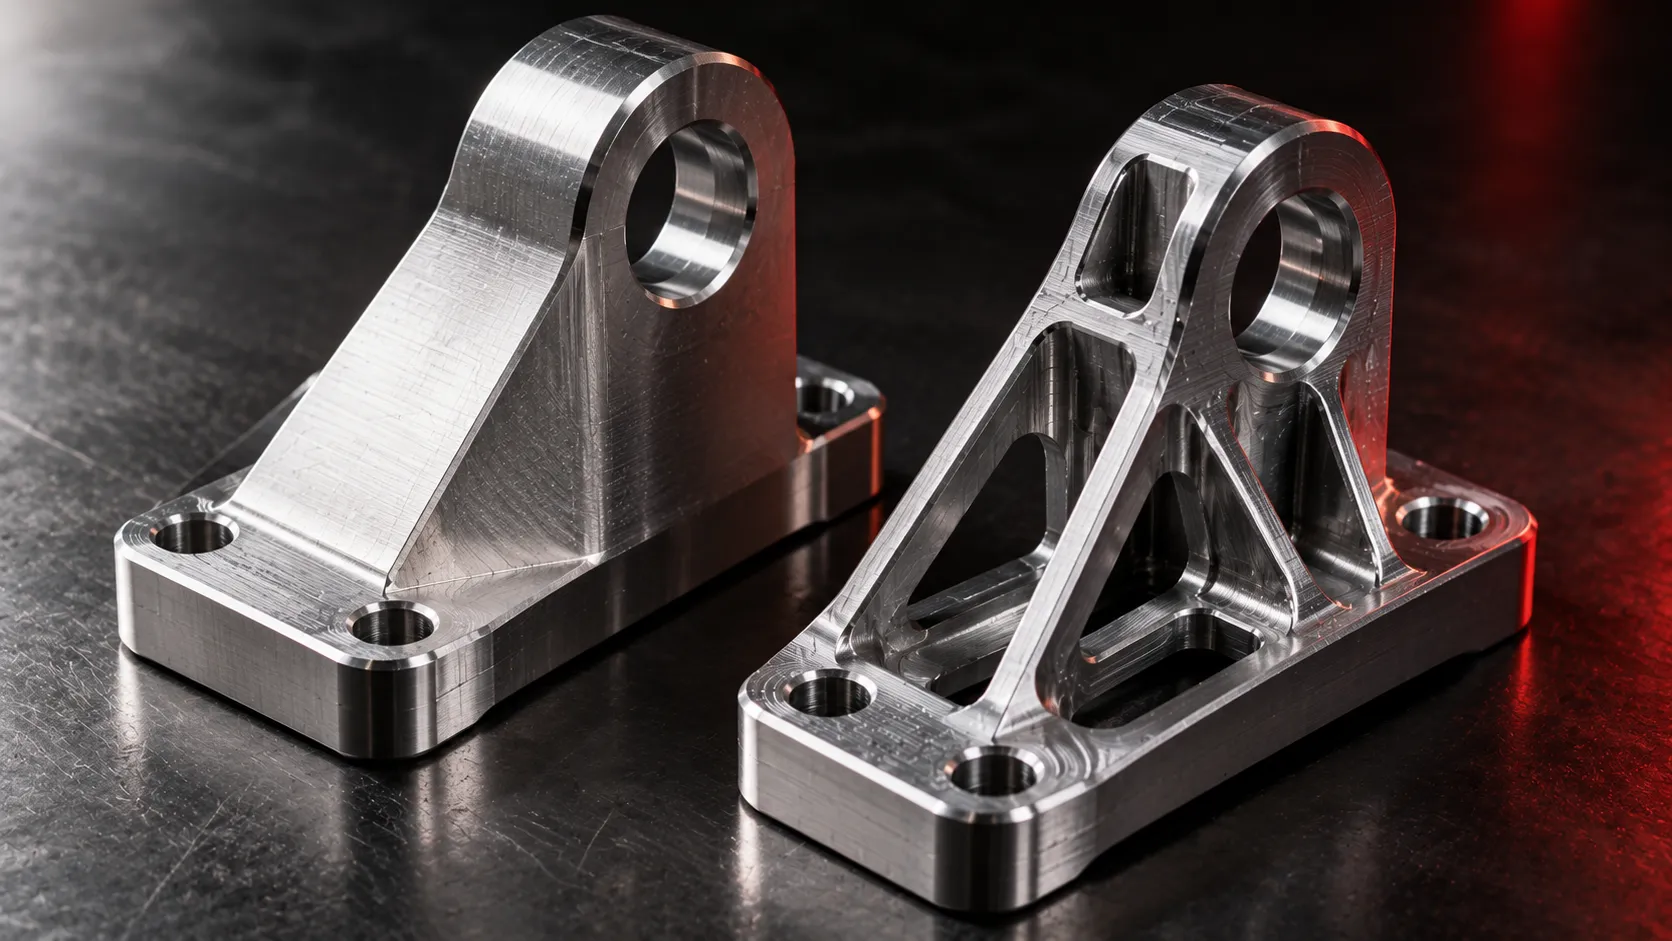
Uniform wall thickness also matters for anything cast or moulded, where uneven walls cause sink marks and warping. If you need a thick section for strength, ribs are almost always better than solid mass.
4. Limit pocket depth relative to width
Deep, narrow pockets are slow and risky. As the depth-to-width ratio increases, the cutter must be longer and thinner, which means less rigidity, more deflection, slower feeds, and worse surface finish.
Where a deep pocket is unavoidable, consider whether the part could be made in two pieces and joined — often cheaper than machining one heroic block.
5. Design around standard components
A custom shoulder bolt might cost many times a standard one, and add weeks of lead time. The same applies to bearings, seals, fasteners, extrusions, and linear rails.
Designing around catalogue components is one of the highest-return habits in machine design. It cuts cost, cuts lead time, and — often overlooked — means your client can source spares locally for the next decade instead of coming back to you for every replacement.
6. Dimension from datums, not in chains
Chained dimensions stack tolerances. If five features are each dimensioned from the previous one, the position of the last feature can drift by the sum of all five tolerance bands — and suddenly nothing fits.
Dimensioning from a common datum keeps the tolerance stack predictable and makes the assembly behave the way your model says it should. It also tells the machinist which surfaces matter, which improves fixturing decisions.
The cheapest part is the one you deleted. Before optimizing a component, ask whether it needs to exist at all.
7. Reduce part count before reducing part cost
This is the rule with the highest leverage, and the one applied least often.
Every part in an assembly carries hidden cost beyond its price: a drawing, a purchase order, an inspection, a stock location, assembly labour, and a potential failure point. Combining two parts into one, or designing a feature out entirely, removes all of that at once.
Before you spend a week shaving cost off a bracket, spend an hour asking whether the bracket is necessary.
The thread running through all seven
Every rule here comes from the same place: the people designing the part and the people making it need to be talking to each other.
When designers never see their drawings machined, they keep repeating the same expensive habits. When machinists never speak to designers, they work around problems silently instead of fixing them at the source.
That feedback loop — not any individual rule — is what keeps manufacturing cost under control. It starts at the quoting stage, which is why what goes into your RFQ matters as much as what goes into the drawing.